FLANGE BLIND prices
October 22, 2026
Industrial Grade B2B Specification
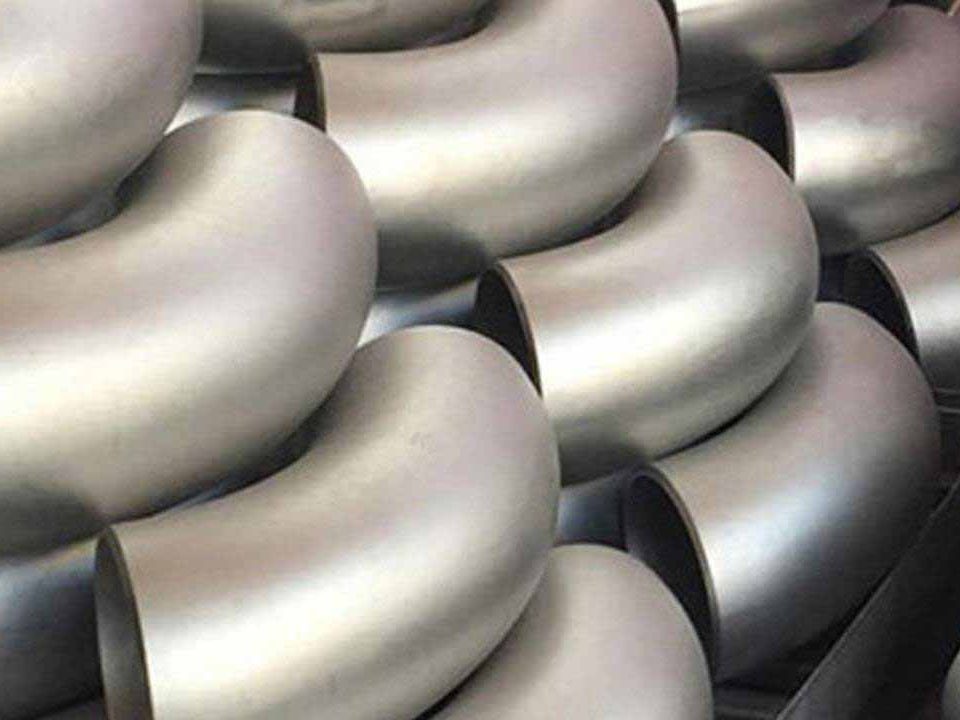
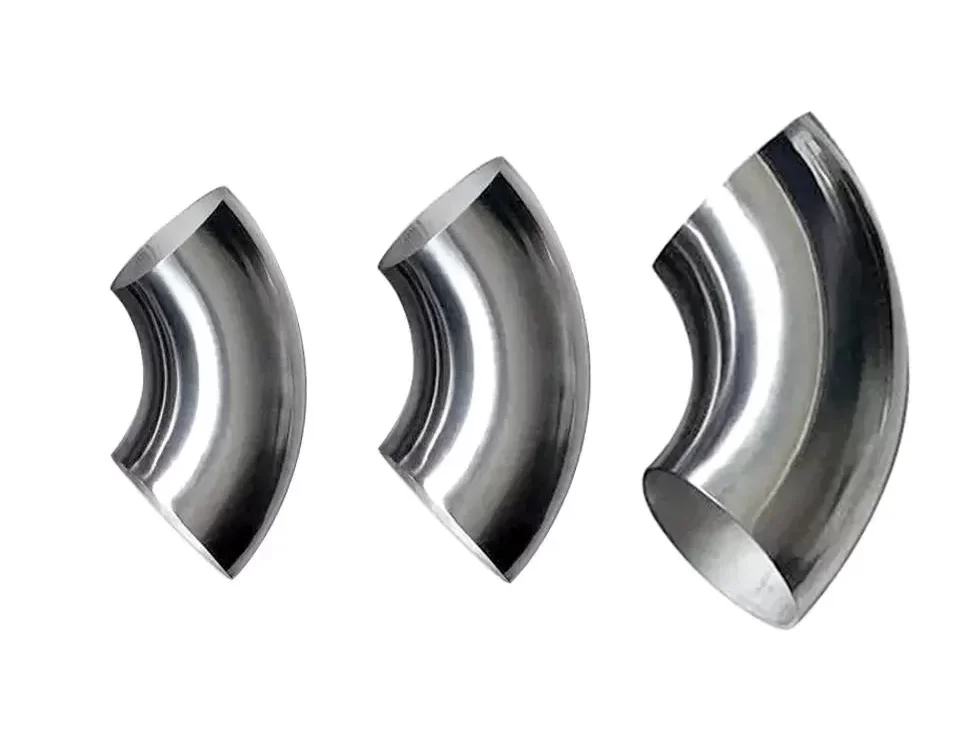
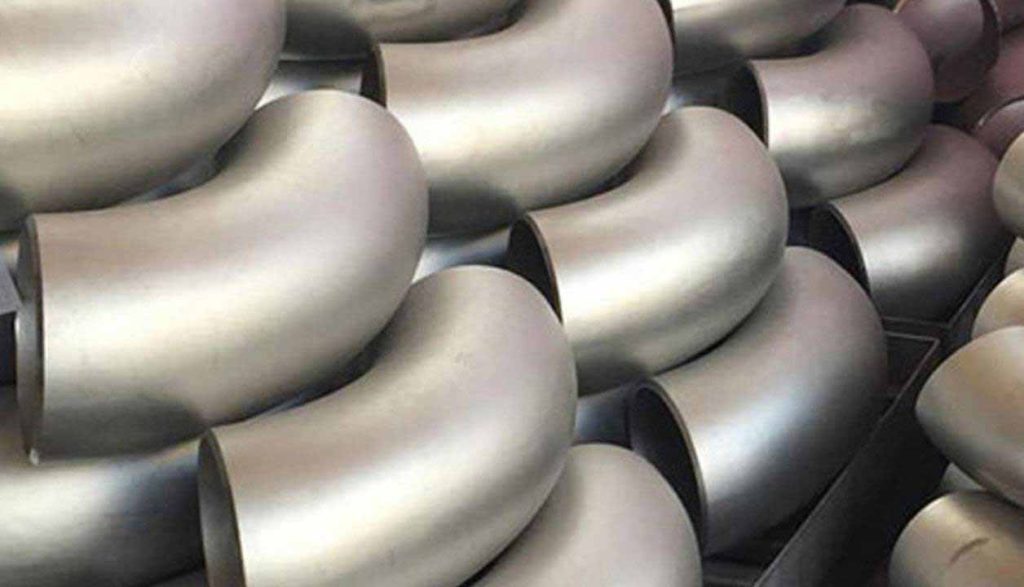
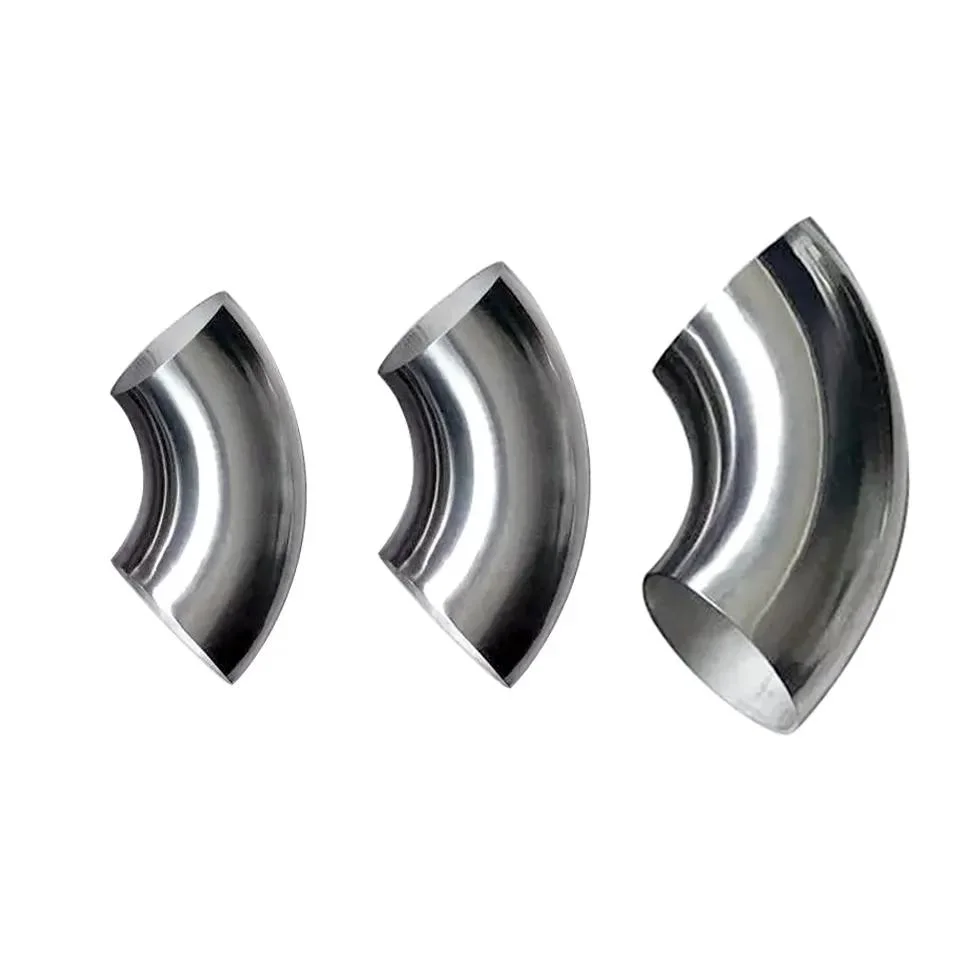
Alloy Steel A234 WP22 Pipe Elbow
ANSI B16.9 | MSS SP 75 | ASME SA234 | Seamless & Welded High-Temperature Chromium-Molybdenum Piping Solutions
Material: ASTM A234 WP22 (2.25Cr-1Mo)
Rating: SCH 10 to XXS
UNS Designation
K31535 (WP22 Cl.1)
Min. Tensile Strength
415 MPa (60 ksi)
Min. Yield Strength
205 MPa (30 ksi)
Molybdenum Content
0.87% – 1.13%
Chromium Content
2.00% – 2.50%
1. General Technical Specifications Matrix
| Parameter | Specification Details |
|---|---|
| Product Name | Alloy Steel Pipe Elbow (Seamless & Welded Buttweld Fittings) |
| Primary Standards | ANSI B16.9, MSS SP 75, ASME B16.28, MSS-SP-43, EN10253-2, DIN2605, GOST17375 |
| Material Grades | ASTM A234 WP22 (Primary focus), WP11, WP5, WP9, WP91, 16Mo3, 10CrMo9-10 |
| Size Range (Seamless) | 1/2″ to 36″ NB (DN15 to DN900) |
| Size Range (Welded) | 26″ to 110″ (Max OD up to 4000mm, 100% X-Ray Welded & Fabricated) |
| Wall Thickness (Schedule) | SCH 5s, 10, 20, 30, STD, 40, 60, 80, 100, 120, 140, 160, XS, XXS |
| Bending Angles | 30°, 45°, 60°, 90°, 180° and custom customized degrees |
| Bending Radius | Short Radius (SR / R=1D) & Long Radius (LR / R=1.5D, 2D, 3D, 5D, 8D, 10D) |
| End Connections | Beveled End (BE), Plain End, Buttweld (BW) |
| Surface Treatment | Sandblasted, Black Painting, Varnished, Anti-Rust Oil Coating |
2. ASTM A234 WP22 Chemical Composition (%)
| Grade | Carbon (C) | Manganese (Mn) | Silicon (Si) | Phosphorus (P) max | Sulfur (S) max | Chromium (Cr) | Molybdenum (Mo) |
|---|---|---|---|---|---|---|---|
| ASTM A234 WP22 | 0.05 – 0.15 | 0.30 – 0.60 | ≤ 0.50 | ≤ 0.040 | ≤ 0.040 | 2.00 – 2.50 | 0.87 – 1.13 |
3. ASME SA234 WP22 Mechanical & Tensile Properties
| Grade / Class | Tensile Strength min (MPa / ksi) | Yield Strength min (MPa / ksi) | Elongation in 2 in. or 50mm min (%) | Max Hardness (Brinell) |
|---|---|---|---|---|
| WP22 Class 1 | 415 – 585 (60 – 85) | ≥ 205 (30) | ≥ 20% | ≤ 248 HBW |
| WP22 Class 3 | 585 – 760 (85 – 110) | ≥ 415 (60) | ≥ 18% | ≤ 290 HBW |
4. ANSI B16.9 Buttweld Fittings Product Line Matrix
| Fitting Category | Available Variants & Configurations | Standard Compliance |
|---|---|---|
| Pipe Elbows | 90° LR/SR, 45° LR, 180° Return Bends, Custom Radius Bends | ASME B16.9 / MSS SP 75 |
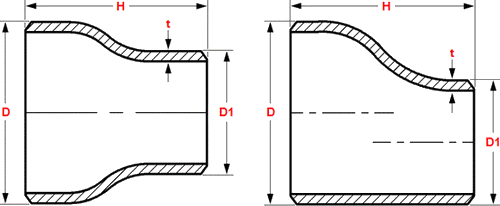
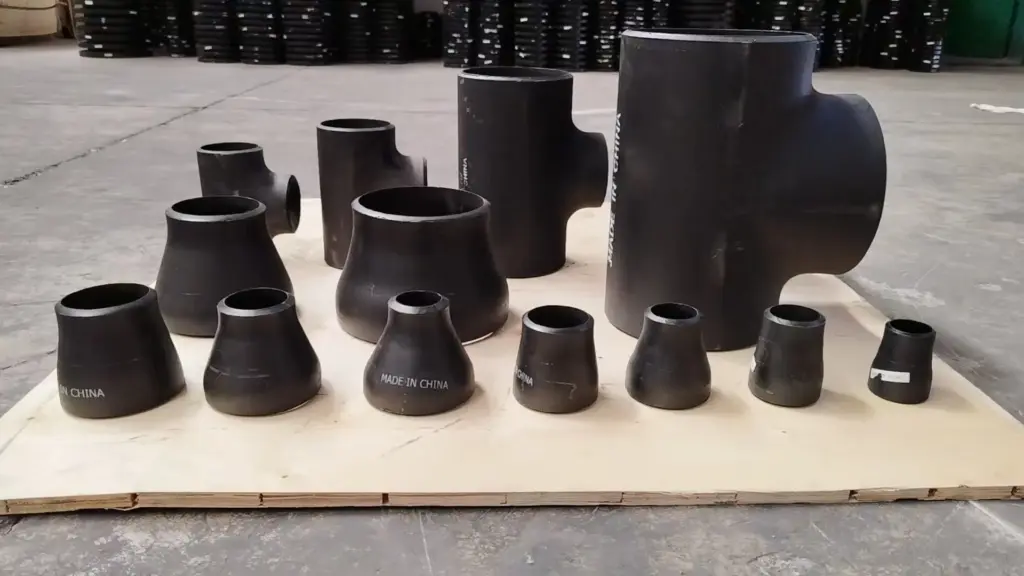
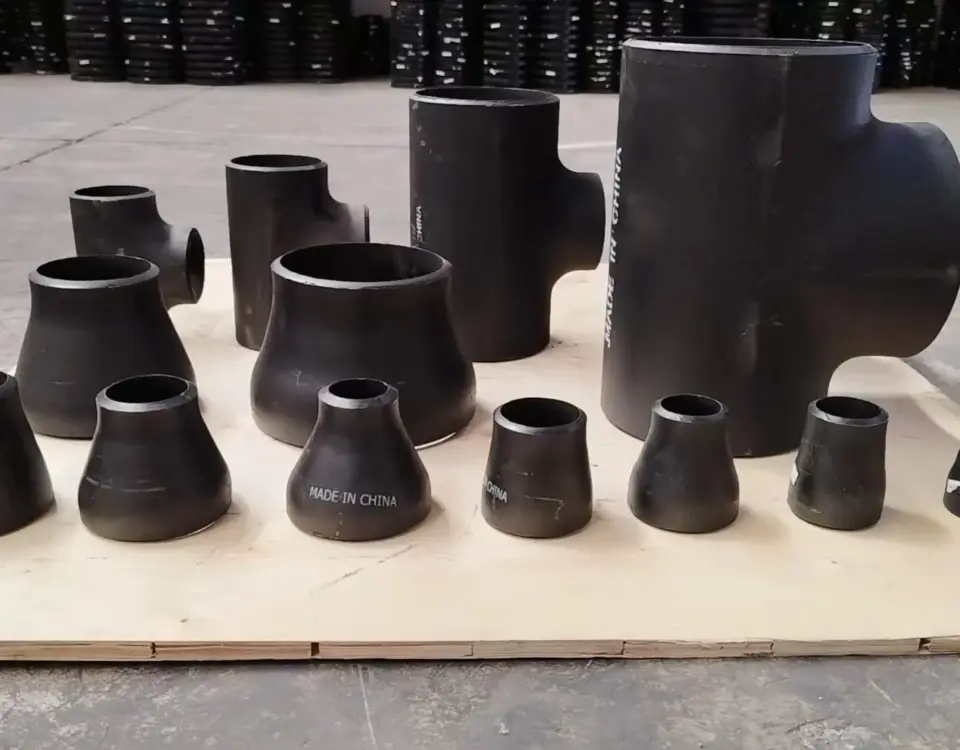
| Reducers | Concentric Reducer, Eccentric Reducer | ASME B16.9 |
| Tees & Crosses | Equal Tee, Reducing Tee, Cross Fitting | ASME B16.9 |
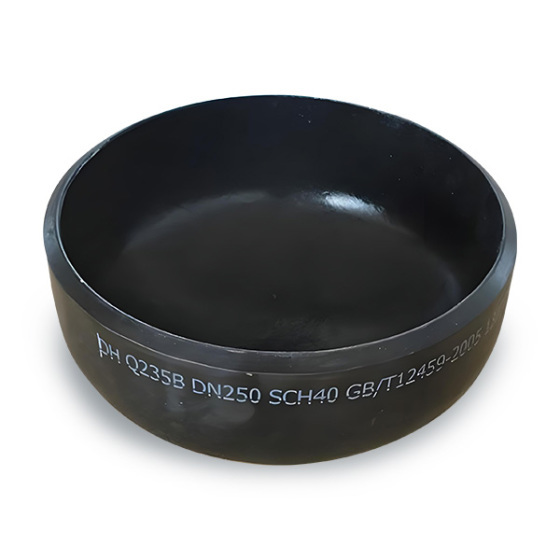
| Pipe Caps & Ends | Pipe Cap, Stub End (Lap Joint) | ASME B16.9 / B16.49 |
5. ASTM A234 Cr-Mo Alloy Steel Grades Comparison
| Grade | UNS Designation | Alloy Type | Typical Application Field |
|---|---|---|---|
| WP1 | K12822 | 0.5Cr – 0.5Mo | Moderate temperature power piping |
| WP11 | K11597 | 1.25Cr – 0.5Mo | Boiler and refinery high-temp lines |
| WP22 | K31535 | 2.25Cr – 1.0Mo | High-pressure hydrogen & steam systems |
| WP5 | K41545 | 5.0Cr – 0.5Mo | Corrosive petroleum refining service |
| WP9 | K90941 | 9.0Cr – 1.0Mo | Severe oxidation-resistant service |
| WP91 | K90901 | 9.0Cr – 1.0Mo – V | Ultra-supercritical power plant boilers |
6. International Equivalent Material Standards Matrix
| Standard Body | Equivalent Grade Specification |
|---|---|
| ASTM / ASME (USA) | ASTM A234 WP22 / ASME SA234 WP22 (Forgings: A182 F22) |
| EN / DIN (Europe) | 10CrMo9-10 (Material No. 1.7380) / EN 10253-2 |
| JIS (Japan) | STPA24 / SFVC FLA22 |
| GOST (Russia) | 12X2MFS / 10Kh2M |
7. Manufacturing Process & Surface Treatment Protocol
Step 1: Hot Forming & Bending
Seamless or welded pipe stock is heated to precise forging temperatures and formed via mandrels or push-benders to achieve exact ANSI B16.9 elbow geometry.
Step 2: Thermal Heat Treatment
Normalized and tempered (or quenched and tempered) strictly per ASTM specifications to ensure grain refinement and mechanical stability.
Step 3: Surface Blasting & Coating
Thorough sandblasting for scale removal, followed by anti-rust oil application, black painting, or varnishing based on project specifications.
8. ASTM A234 WP22 Heat Treatment Requirements
| Treatment Type | Temperature Parameter | Cooling Medium / Method |
|---|---|---|
| Full Annealing | 900°C – 950°C (1650°F – 1740°F) | Furnace slow cooling |
| Normalizing & Tempering | Normalize at 900°C min; Temper at 700°C min | Air cooling / controlled furnace cooling |
| Post-Weld Heat Treatment (PWHT) | 670°C – 740°C (1250°F – 1365°F) | Controlled cooling in still air |
9. Quality Control, Inspection & Testing Standards
| Inspection Item | Testing Method / Standard | Acceptance Criteria |
|---|---|---|
| Dimensional Verification | Vernier calipers, laser meters, radius gauges | Strict compliance with ANSI B16.9 / MSS SP 75 |
| Wall Thickness Tolerance | Ultrasonic thickness testing (UT) | Minimum thickness not less than 87.5% (-12.5%) |
| Positive Material Identification | PMI Analyzer (XRF Spectroscopy) | Verification of Cr (2.25%) and Mo (1.0%) ranges |
| Non-Destructive Examination | Magnetic Particle (MT), Ultrasonic (UT), X-Ray Radiography | Zero cracks, lack of fusion, or injurious defects |
| Certification | Material Test Certificate (MTC) | EN 10204 3.1 / 3.2 Certified by Third Party (TUV, SGS, BV) |
10. Industrial Application Sectors & Operating Environments
| Industry Sector | Specific Piping System / Unit | Operating Conditions |
|---|---|---|
| Petrochemical & Refining | Hydrogenation units, hydrocrackers, catalytic reformer feed lines | High temperature, high pressure, high hydrogen partial pressure |
| Power Generation | Subcritical & supercritical boiler main steam piping, reheat lines | Elevated temperatures up to 600°C (1110°F) |
| Oil & Gas Pipelines | High-pressure transmission lines, sour gas/oil gathering stations | MSS SP 75 pipeline networks, heavy wall requirements |
| Coal Chemical Processing | Gasification reactor effluent lines, synthesis gas piping | Corrosive gas streams and abrasive particulate service |
11. High-Temperature Hydrogen Service (API RP 941 Compliance)
ASTM A234 WP22 alloy steel elbows are specifically favored in hydrogen-rich refinery environments due to the addition of Molybdenum and Chromium, which prevent hydrogen attack and decarburization.
| Design Parameter | Engineering Requirement & Limit |
|---|---|
| Max Operating Temperature | Up to 550°C to 600°C per Nelson Curves for 2.25Cr-1Mo steels |
| Weldability & Preheat | Requires preheating (150°C–200°C) and mandatory PWHT to prevent cracking |
12. ANSI B16.9 Elbow Center-to-Face Dimensions Reference
| Nominal Pipe Size (NPS) | Outside Diameter (mm) | 90° LR Center-to-Face (A) | 90° SR Center-to-Face (B) | 45° LR Center-to-Face (C) |
|---|---|---|---|---|
| 1/2″ | 21.3 | 38 mm | 25 mm | 16 mm |
| 1″ | 33.4 | 38 mm | 25 mm | 22 mm |
| 2″ | 60.3 | 76 mm | 51 mm | 35 mm |
| 4″ | 114.3 | 152 mm | 102 mm | 64 mm |
| 8″ | 219.1 | 305 mm | 203 mm | 124 mm |
| 12″ | 323.8 | 457 mm | 305 mm | 178 mm |
13. Packaging, Marking & Export Compliance
| Logistics Parameter | Standard Export Specification |
|---|---|
| Surface Protection | Anti-rust oil coated, plastic caps fitted on both bevel ends to protect edges |
| Packaging Type | Sturdy fumigated wooden boxes, wooden pallets, or waterproof woven bags |
| Product Marking | Stamped with Grade (WP22), Heat No., Size, Schedule, Standard (ANSI B16.9) |
14. Key Supply Advantages & Ready Stock Benefits
Ready Stock
Extensive inventory of standard sizes (1/2″ to 24″) ready for immediate dispatch.
Fast Delivery
Streamlined manufacturing lines ensure rapid lead times for custom orders.
Custom Fabrication
Specialized wall thicknesses, radii, and non-standard angles built to print.
15. Frequently Asked Technical Questions (FAQ)
| Technical Query | Expert Answer / Specification Guideline |
|---|---|
| What is the main advantage of WP22 over carbon steel? | WP22 contains 2.25% Chromium and 1% Molybdenum, providing superior creep resistance and strength at temperatures up to 600°C. |
| Are ASTM A234 WP22 elbows weldable on site? | Yes, but they require preheating and strict Post-Weld Heat Treatment (PWHT) to prevent micro-cracking and brittleness. |
| What standards govern these elbows? | Manufactured strictly to ASME/ANSI B16.9 for dimensions and ASTM A234 for material properties. |
16. Nominal Weight Reference Table (ANSI B16.9 90° Long Radius Elbows)
Theoretical weight values in kilograms (kg) for Alloy Steel A234 WP22 90° LR elbows across standard wall schedules.
| NPS (Inches) | DN | SCH 40 / STD (kg) | SCH 80 / XS (kg) | SCH 120 (kg) | SCH 160 (kg) | SCH XXS (kg) |
|---|---|---|---|---|---|---|
| 2″ | 50 | 0.89 | 1.20 | – | 1.90 | 2.40 |
| 3″ | 80 | 2.20 | 3.00 | – | 4.40 | 5.60 |
| 4″ | 100 | 4.30 | 6.00 | 8.10 | 9.80 | 12.20 |
| 6″ | 150 | 12.00 | 16.80 | 22.50 | 28.60 | 34.50 |
| 8″ | 200 | 24.80 | 35.20 | 49.00 | 63.50 | 71.00 |
| 10″ | 250 | 43.50 | 62.00 | 88.00 | 115.00 | 130.00 |
| 12″ | 300 | 68.00 | 96.50 | 136.00 | 180.00 | 205.00 |
| 14″ | 350 | 92.00 | 132.00 | 185.00 | 245.00 | 280.00 |
| 16″ | 400 | 124.00 | 180.00 | 252.00 | 335.00 | 385.00 |
| 24″ | 600 | 310.00 | 450.00 | 640.00 | 860.00 | 990.00 |
17. MSS SP 75 WPHY Material Grades Specifications
High-test wrought butt-welding fittings designed for high-pressure oil and gas transmission systems.
| MSS SP 75 Grade | Min Yield Strength (MPa / ksi) | Min Tensile Strength (MPa / ksi) | Carbon Equivalent (CE) max |
|---|---|---|---|
| WPHY 42 | 290 (42) | 415 (60) | 0.40% |
| WPHY 52 | 360 (52) | 460 (66) | 0.42% |
| WPHY 60 | 415 (60) | 520 (75) | 0.43% |
| WPHY 65 | 450 (65) | 535 (77) | 0.45% |
| WPHY 70 | 485 (70) | 565 (82) | 0.45% |
18. ASME B16.9 Dimensional Tolerances for Buttweld Elbows
| Nominal Size (NPS) | Outside Diameter (At Bevel) | Inside Diameter (At End) | Center-to-End Dimension (A, B, C) | Off Alignment / Squareness |
|---|---|---|---|---|
| 1/2″ to 2-1/2″ | +1.6 mm / -0.8 mm | ±0.8 mm | ±2.0 mm | 1.0 mm |
| 3″ to 3-1/2″ | ±1.6 mm | ±1.6 mm | ±2.0 mm | 2.0 mm |
| 4″ | ±1.6 mm | ±1.6 mm | ±2.0 mm | 2.0 mm |
| 5″ to 8″ | +2.4 mm / -1.6 mm | ±1.6 mm | ±2.0 mm | 4.0 mm |
| 10″ to 18″ | +4.0 mm / -3.2 mm | ±3.2 mm | ±2.0 mm | 5.0 mm |
| 20″ to 24″ | +6.4 mm / -4.8 mm | ±4.8 mm | ±2.0 mm | 6.0 mm |
19. Welding Bevel End Specifications (ANSI B16.25 Compliance)
All A234 WP22 buttweld elbows feature precision machined bevel ends in compliance with ASME B16.25 for sound field root pass welding.
Wall Thickness t ≤ 22mm (0.88″)
Plain Bevel: Angle 37.5° ± 2.5°, Root Face 1.6mm ± 0.8mm (1/16″ ± 1/32″). Standard straight bevel contour.
Wall Thickness t > 22mm (0.88″)
Compound Bevel: Angle 37.5° ± 2.5° outer, 10° ± 1.0° inner transition bevel. Reduces weld metal volume requirement.
20. ASTM A234 Supplementary Requirements (S1 – S8)
| Code | Supplementary Test Requirement | Engineering Objective |
|---|---|---|
| S1 | Product Analysis (Check Analysis) | Verifies individual chemical heat composition of finished fitting. |
| S2 | Tension Test | Confirms room temperature yield/tensile per heat treatment lot. |
| S3 | Liquid Penetrant Examination (PT) | Detects surface defects, laps, or cracks on outer/inner surfaces. |
| S4 | Magnetic Particle Examination (MT) | Identifies sub-surface flaws in ferromagnetic alloy structures. |
| S5 | Hydrostatic Testing | Pressure verification matching 1.5x straight pipe rating. |
| S7 | Charpy V-Notch Impact Test | Evaluates low-temperature or notch toughness property. |
Technical Assistance & Custom Piping Solutions
Need custom radii (3D, 5D, 8D), heavy wall SCH XXS WP22 elbows, or third-party inspection (SGS/TUV) for your project?
Consult Engineering Team

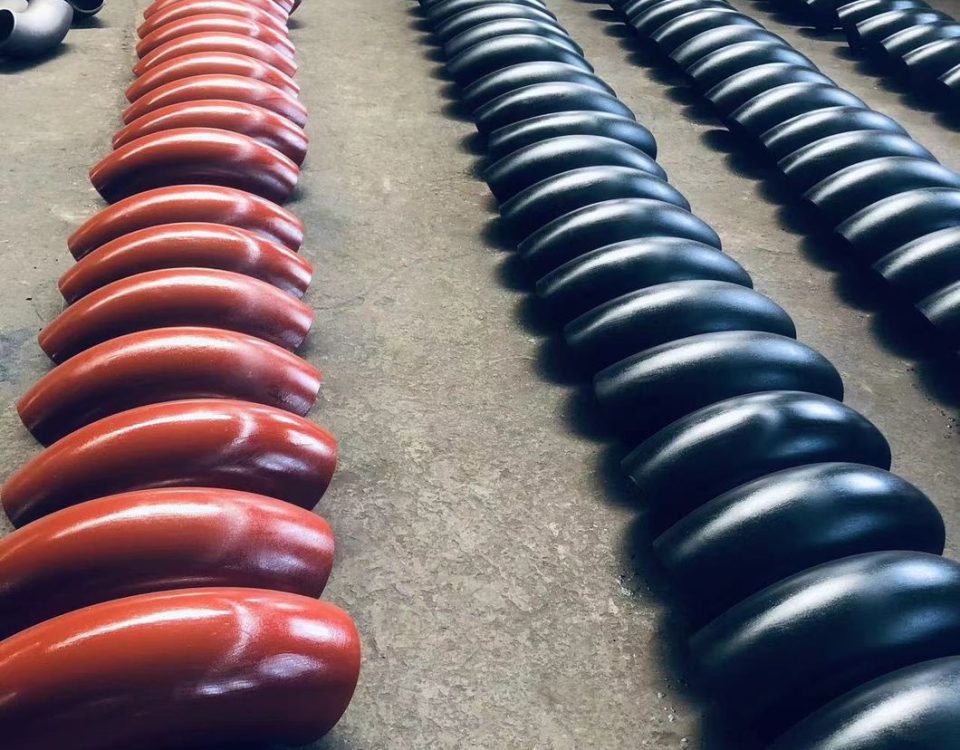
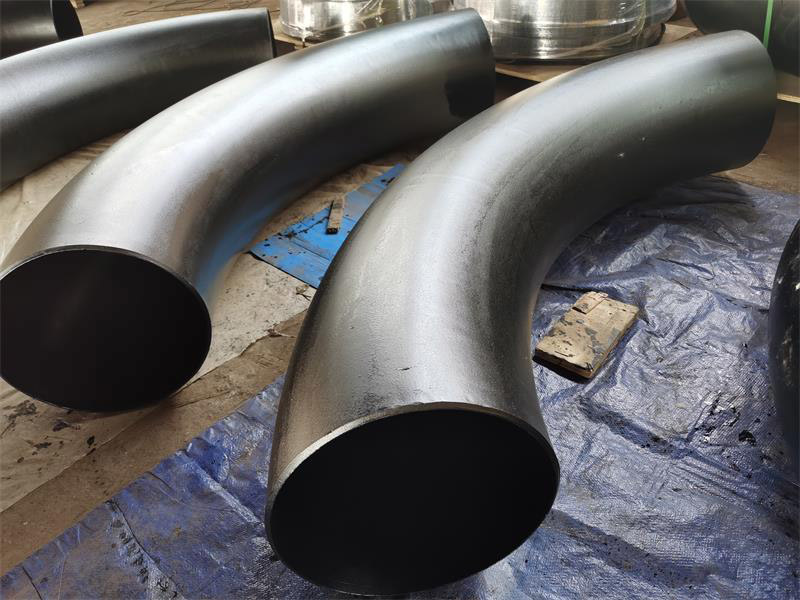
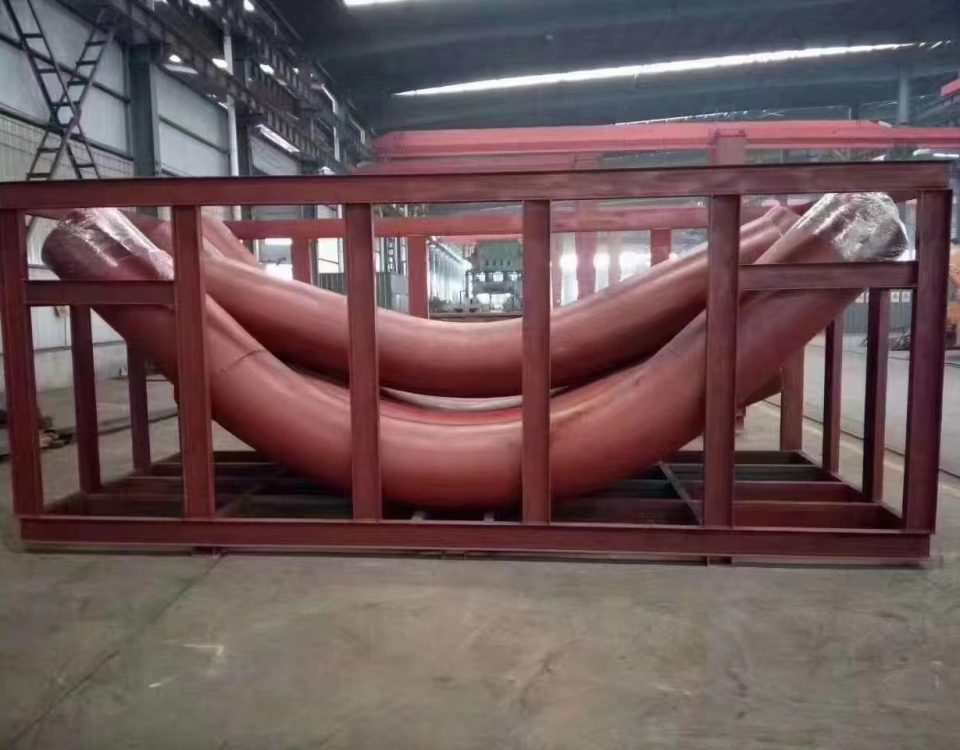
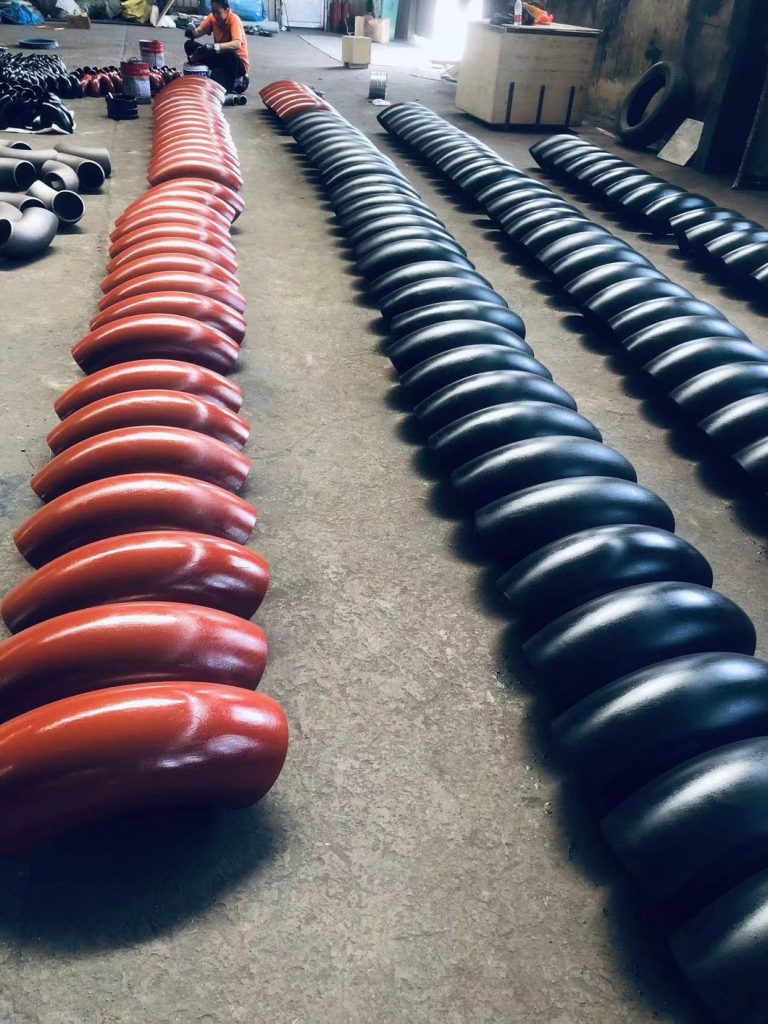
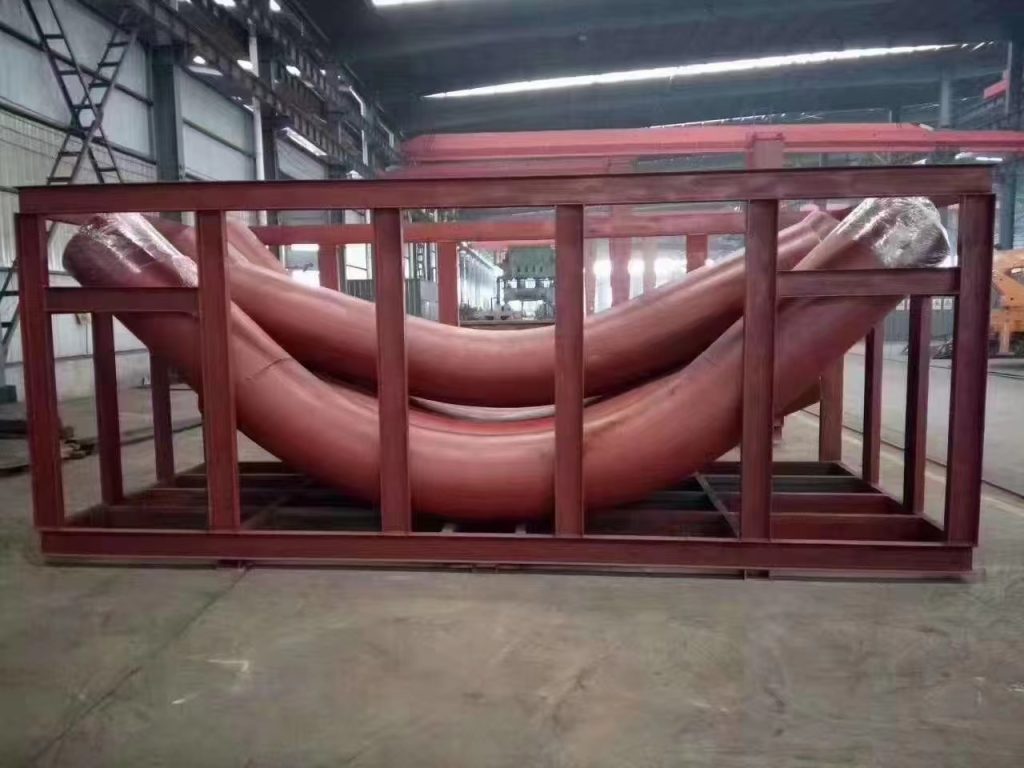
Induction bends come in standard bend angles (e.g. 45°, 90°, etc.) or can be custom made to specific bend angles. Compound bends (out-of-plane) bends in a single joint of pipe can also be produced. The bend radius is specified as a function of the diameter. For example, common bend radii for induction bends are 3D, 5D and 7D, where D is the nominal pipe diameter.